Engineering solution
Wear and Friction: Ceramic Components for the Requirement
Where metal surfaces keep failing: sliding wear, abrasion, galling and erosion. The fix is usually a change of material at one interface, not a redesign of the machine.
The engineering problem
What is actually failing
A metal component wears out on a predictable cycle, and replacing it has become a maintenance item rather than an exception. Sometimes the wear is abrasive, sometimes it is galling between two similar metals, and sometimes it is erosion by a particle-laden stream.
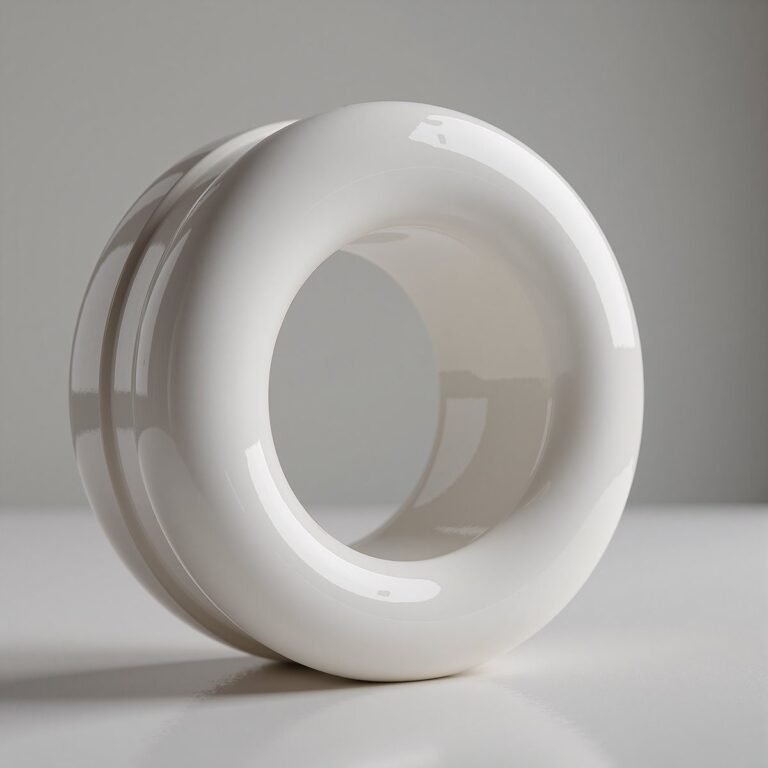
Bushings and guide elements are the parts this problem most often lands on; their bore, fit and finish requirements are on the ceramic bushings page. Where the wear is erosion rather than sliding contact, the part is usually a nozzle, and those are covered under ceramic nozzles. Seal faces and wear rings that fail by the same sliding mechanism are produced as rings and seal rings.
What the part has to deliver
These are the parameters that decide the material. Not all of them matter equally, which is why the dominant one is identified first.
| Requirement | What it governs |
|---|---|
| Hardness | Higher than the abrasive or the counterface it runs against |
| Fracture toughness | Enough to survive shock and edge loading without chipping |
| Surface finish | Low enough Ra to control friction at the running surface |
| Chemical compatibility | Unaffected by the medium carrying the abrasive |
| Thermal stability | Retains hardness at the service temperature |
Options and the reason behind each
Where two requirements conflict, the trade-off is explained before quoting rather than after.
| Material | Why it is chosen here |
|---|---|
| Alumina (Al2O3) | General-purpose wear resistance at moderate cost; the default for chutes, liners and guide parts |
| Zirconia (ZrO2) | Where impact is present as well as sliding wear; highest toughness avoids the chipping that rules out harder options |
| Silicon carbide (SiC) | Abrasion and erosion at high velocity, especially with heat or chemical attack present |
| Silicon nitride (Si3N4) | Cycled mechanical load combined with thermal movement |
What the choice costs in production
These are the constraints that turn a material decision into a manufacturing route, and sometimes into a design change.
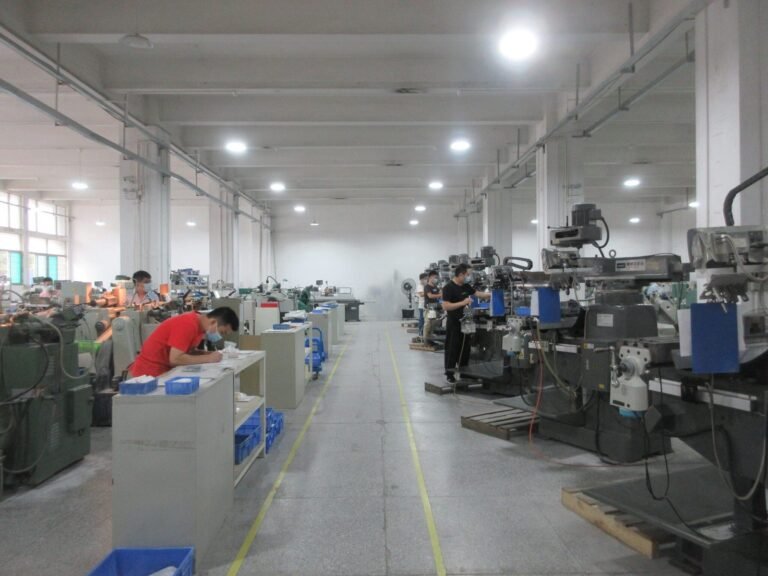
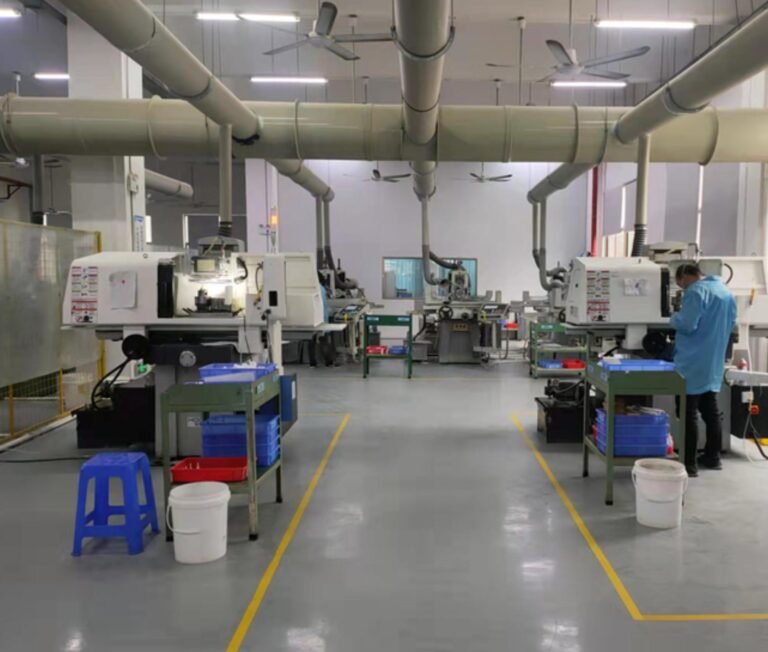
- Hardness makes removal slow: diamond grinding is the only route, and it sets both cost and lead time
- Sharp edges chip under load, so an edge break is specified as a functional requirement rather than a finishing detail
- A lapped or polished surface adds steps but directly controls friction at the running face
- Insert design often reduces cost: a small ceramic wear insert in a metal carrier is cheaper than a fully ceramic part
- Counterface pairing matters as much as the ceramic itself, since ceramic against a soft metal can wear the metal instead
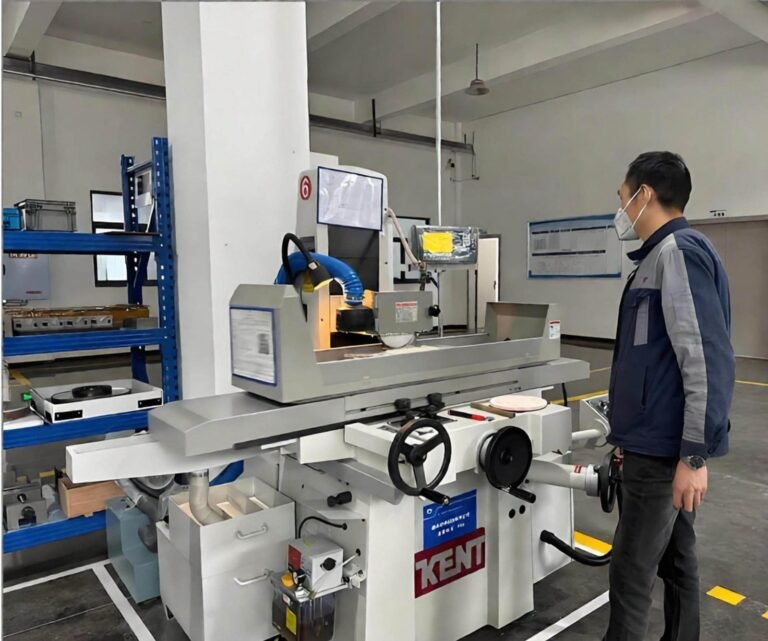
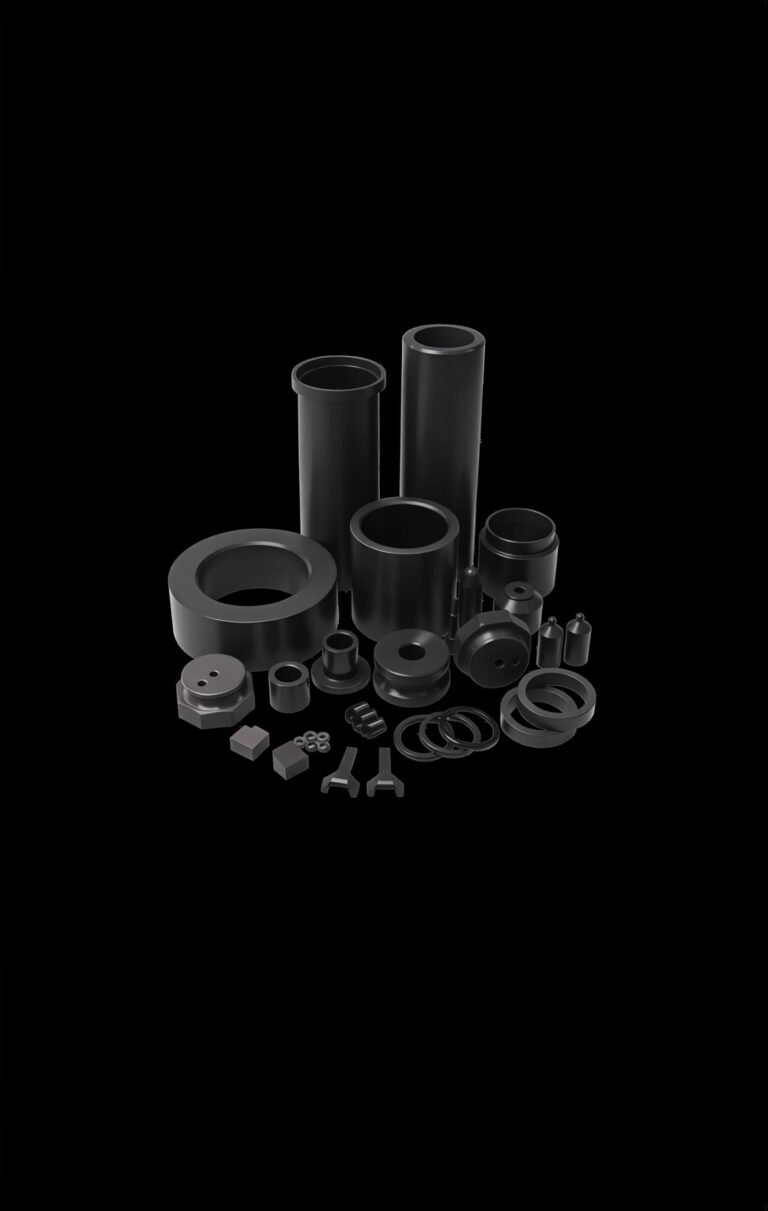
Capabilities depend on material, geometry, feature size and finishing requirements. Critical dimensions are reviewed against the drawing.
Where this solution is applied
Indicative component types. No customer names are published, and no application is described that we have not made.
Wear plates, liners and chute components in material handling
Pump plungers, sleeves and valve seats
Nozzles for abrasive blasting and slurry service
Bushings and guide elements in production machinery
Wire and thread guides in textile and wire drawing equipment
How the result is verified
The inspection plan is agreed before machining, since ceramic cannot be reworked the way metal can.
- Surface roughness on the running face
- Flatness and parallelism for wear plates in sliding contact
- Edge condition against an agreed chip criterion
- Hardness and density verification through the material certificate
The part and the process
Frequently asked
Describe the problem and send the drawing
The requirement decides the material. Give the conditions and the review will state which material and route apply, and why.