Engineering guide
Ceramic Machining Tolerance Guide
Which tolerances are realistic on which features, why a deep thin pocket cannot hold what a flat face can, and how to place tolerance callouts so the price reflects the function.
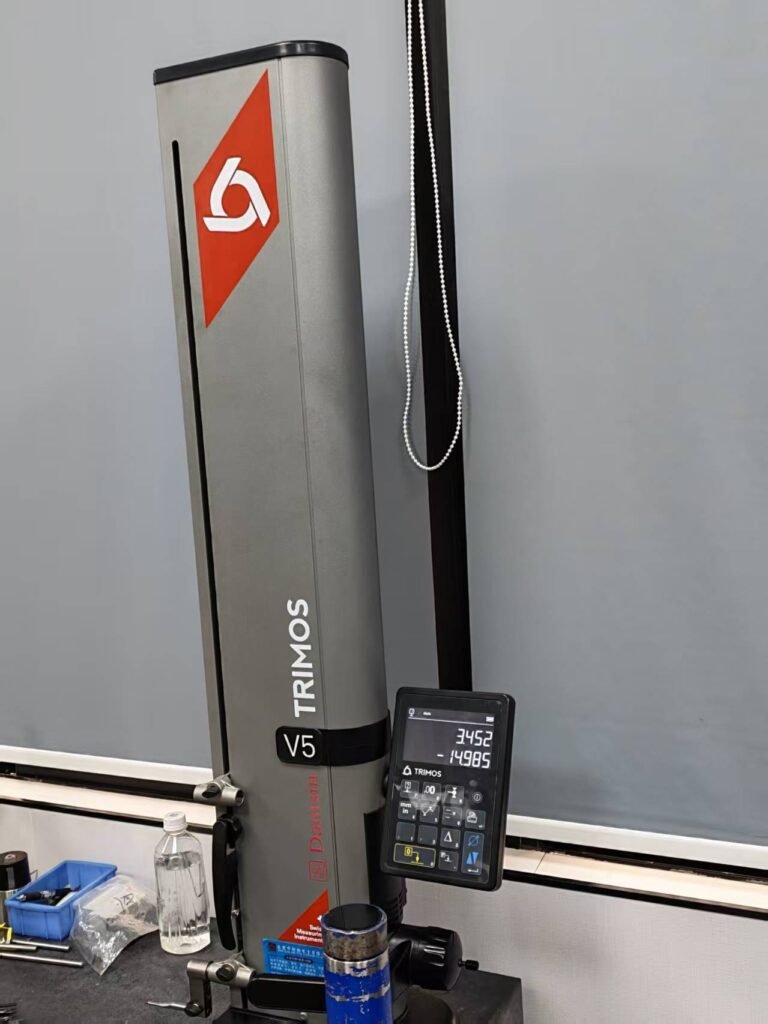
Capability
The confirmed figures and what they apply to
These are feature-specific values, not a general tolerance for every dimension on a part.
Diamond-ground bores hold a hole diameter tolerance of 0.003 mm, and ground cylindrical and bore features hold roundness of 0.0005 mm. Opposed faces on plates, rings and blocks hold parallelism of 0.002 mm, and slots and narrow features produced by diamond grinding run down to a minimum slot width of 0.2 mm. Each figure belongs to the feature named beside it; none of them is a general tolerance for a whole drawing. Reachability on a specific part is confirmed from the engineering drawing, because the achievable value moves with the ceramic material, the part geometry, the feature size, the wall thickness and the machining process.
- 1Hole diameter0.003 mm
- 2Parallelism0.002 mm
- 3Roundness0.0005 mm
- 4Minimum slot width0.2 mm
The same figures on a logarithmic scale. Three of them sit inside one decade and the fourth is two decades further out, which is the part of a capability the numbers alone do not convey.
Actual achievable precision depends on ceramic material, geometry, feature size, machining route and drawing requirements. Final capability is subject to engineering review.
Bores that have to hold roundness and fit a mating shaft are covered by the ceramic bushings family. Which industries call for these tolerances, and what drives them, is set out on the industry pages. Where flatness and parallelism are called out against a datum rather than on the feature alone, the application is covered under precision alignment components. A tolerance only means the same thing to both sides once the measurement method is agreed, because one feature measured in two ways can report two different values and both be correct; how the method, the datum scheme and the sampling plan are fixed is set out under precision ceramic inspection methods.
Why the same tolerance is not available everywhere
The material is hard and brittle, so the achievable tolerance depends on how the tool reaches the feature.
| Feature | Why it differs from a flat face |
|---|---|
| Flat ground surface | Best case: rigid setup, full support |
| Long small bore | Tool deflection rises with depth |
| Deep narrow pocket | Limited by tool diameter and chip clearance |
| Thin wall | Deflects under clamping and grinding load |
| Slot close to an edge | Edge chipping risk |
| Long slender shaft | Deflection over the length sets straightness |
How to call out tolerance so it costs less
Tolerance the function, not the part.
- Tolerance the mating and sealing faces individually
- Reference the datum face that the manufacturing setup can use
- Leave non-functional dimensions at a general class
- Avoid tolerancing both faces of a thin wall
- State whether a callout is functional or nominal
Metal tolerances do not transfer directly
A tolerance routinely held on a machined aluminium part may be achievable in ceramic and still be the wrong callout, because the cost structure is different.
| Situation | Effect |
|---|---|
| Tight tolerance in alumina | Reachable by grinding; moderate cycle-time impact |
| Tight tolerance in silicon carbide | Reachable; large cycle-time impact and higher cost |
| Tight tolerance on a thin wall | Risk of chipping and distortion; may be unachievable |
| Tight parallelism across a thin plate | Limited by part thickness, not by the machine |
| Tight tolerance on a micro feature | Limited by tool survival, not by positioning accuracy |
Where the work is done
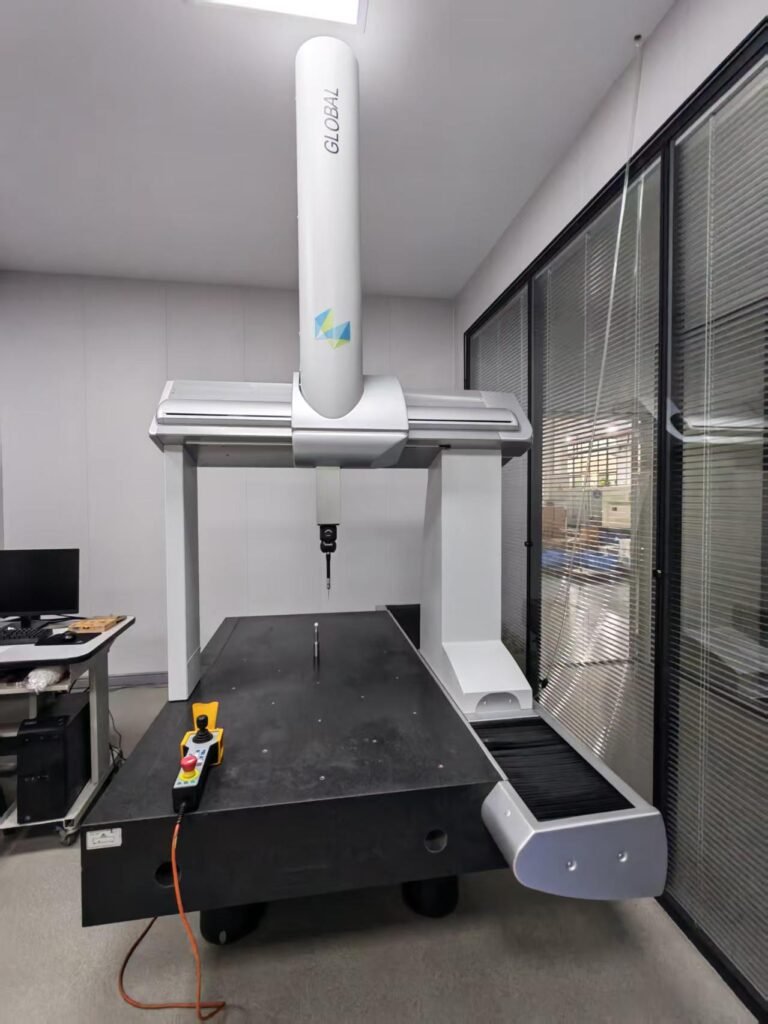
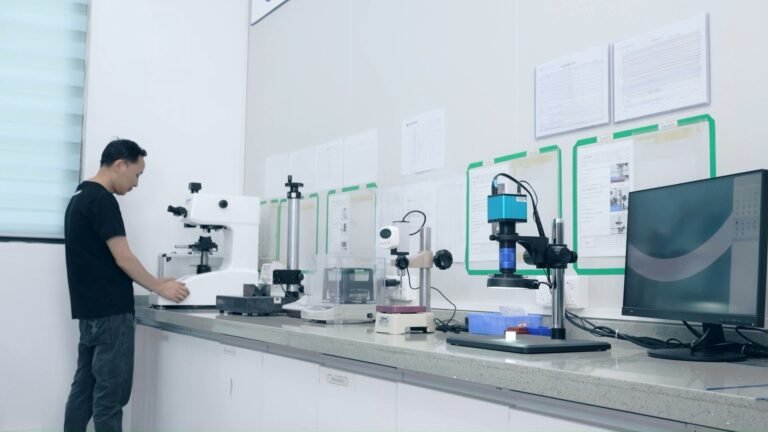
Frequently asked
Can you hold 0.003 mm on any feature?
The confirmed hole diameter tolerance is 0.003 mm and roundness 0.0005 mm. Whether a specific feature reaches it depends on the material, geometry and accessibility, and it is confirmed from the drawing.
Why is a tight tolerance on a deep pocket a problem?
The tool has to be thin enough to enter and rigid enough to cut. Those two requirements conflict, and the depth-to-width ratio is where the conflict becomes a limit.
Does a finer tolerance always cost more?
It costs more in grinding time, which is the dominant cost in ceramic machining. Removing a tolerance that was not functional is usually the cheapest form of cost reduction.
How do I know a tolerance is achievable before ordering?
Send the drawing. The engineering review states what is achievable on each feature before a price is issued.
Have a drawing that this guide applies to?
Send it with the material and the quantities. The review confirms what is achievable before any price is issued.