Material selection
Machinable Ceramics (machinable glass-ceramic) for Custom Precision Components
The one technical ceramic on this page that is cut with conventional tooling instead of diamond. It is chosen when the geometry has to be proved quickly, or when the quantity is too small to justify a grinding route.
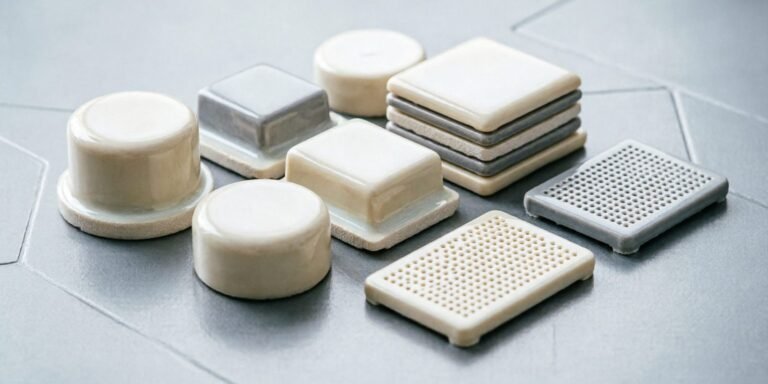
Material overview
What is machinable glass-ceramic?
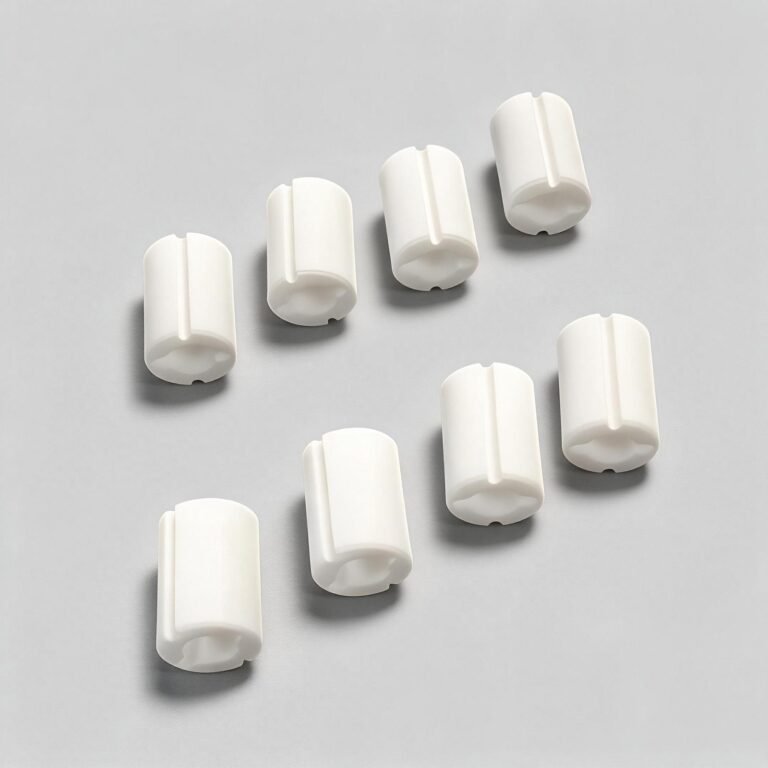
A machinable glass-ceramic is a polycrystalline ceramic whose microstructure is engineered so it can be machined with conventional carbide tooling, with no firing step after machining. Published typical values for the grade supplied are a flexural strength of 108 MPa, a maximum use temperature of 800 °C and a thermal conductivity of 1.71 W/m·K. It is specified when geometry has to be proved quickly, when deep small features would be impractical to grind, or when the quantity is too small to justify a diamond grinding route.
When to choose Machinable Ceramics
Each row links a published property to the engineering benefit it buys and the condition where that benefit is the reason for the choice.
| Property | Engineering benefit | Relevant application condition |
|---|---|---|
| Machinable with carbide tooling | Short lead time with no firing step | Prototypes and one-off fixtures |
| Gas permeability published as zero for this grade | Suits vacuum service | Vacuum chambers and feedthroughs |
| Dielectric strength 30 kV/mm | Reliable insulation in small sections | High-voltage insulators and spacers |
If your project looks like one of these
- Prototypes and first articles where the geometry is not yet frozen
- Fixtures, insulators and spacers in ones and twos
- Vacuum, analytical and laboratory components where outgassing and permeability matter
- Parts with deep small features that would be impractical to grind
- Bushings and standoffs where moderate wear resistance is enough
Where a grade is machined rather than ground, the route is described in complex geometry, and the step from first article to series under prototype to production. The drawing requirements that decide the result are listed in how to specify a custom ceramic part drawing. Boron nitride is the related grade in this group.
Machinable Ceramics typical properties
Representative published values for material selection. Where a property governs the design, state it on the drawing so it is confirmed against the supplied batch.
| Property | Typical value |
|---|---|
| Colour | White |
| Density (g/cm³) | 2.6 |
| Gas permeability (published) | 0 |
| Water absorption (%) | 0.00 |
| Rockwell hardness R45N | 40 |
| Vickers hardness, 500 g (GPa / kg/mm²) | 11.5 / 1175 |
| Elastic modulus, 25 °C (GPa) | 65 |
| Flexural strength, 20 °C (MPa) | 108 |
| Compressive strength, 20 °C (MPa) | 488 |
| Maximum use temperature (°C) | 800 |
| Thermal conductivity, 25 °C (W/m·K) | 1.71 |
| Thermal expansion coefficient (×10⁻⁶/K) | 7.2 |
| Thermal shock resistance (ΔT, °C) | 200 |
| Dielectric strength (kV/mm) | 30 |
| Volume resistivity, 20 °C (Ω·cm) | 1016 |
Material properties are representative and grade-dependent. Final material selection should be confirmed against the specific grade and application conditions. The inspection certificate for the batch supplied is the governing document for a delivered order.
Machinable Ceramics against Alumina
Strength in bending and heat removal separate the range faster than any other pair of properties. Each bar is the range published for that material family, taken from the same comparison table that appears in the selection centre.
Flexural strength, MPa
- Alumina (Al2O3), 95-99.7%300 – 380
- Machinable glass-ceramic108
A longer bar carries more load before it breaks. A range covers the grades supplied in that family rather than one nominal figure.
Source: Flexural strength (MPa)
Thermal conductivity, W/m·K
- Alumina (Al2O3), 95-99.7%20 – 32
- Machinable glass-ceramic1.71
A longer bar moves heat away faster. Conducting heat while still insulating electrically is the pairing power electronics needs, and it is why this property is read next to strength.
Source: Thermal conductivity (W/m·K)
Why engineers select it
Each of these is a reason to choose it. The limitations that follow are the reason not to.
Machined with carbide tooling at conventional speeds, so no diamond grinding step is needed and the lead time is short
Gas permeability published as zero and 0.00% water absorption for this grade, which suits vacuum and analytical equipment
Good electrical insulation, with a dielectric strength of 30 kV/mm and volume resistivity of 1016 Ω·cm
Machinable to fine internal detail that would be slow and expensive to reach by grinding
Low thermal conductivity of 1.71 W/m·K, so it also works as a thermal break
What it is not good at
Stating this up front prevents a material being selected for the one thing it cannot do.
Flexural strength of 108 MPa is a fraction of alumina or zirconia, so it is not a load-bearing material
Maximum use temperature of 800 °C is the lowest of the common engineering ceramics
Hardness of R45N 40 means it wears quickly in sliding contact against harder materials
It is a glass-ceramic, so it is not used where chemical resistance to strong alkalis is required
What the material costs in production
The material decision and the manufacturing route are the same decision seen from two ends. Green machining, diamond grinding, lapping and polishing each have a place, and the route depends on the geometry and the tolerance.
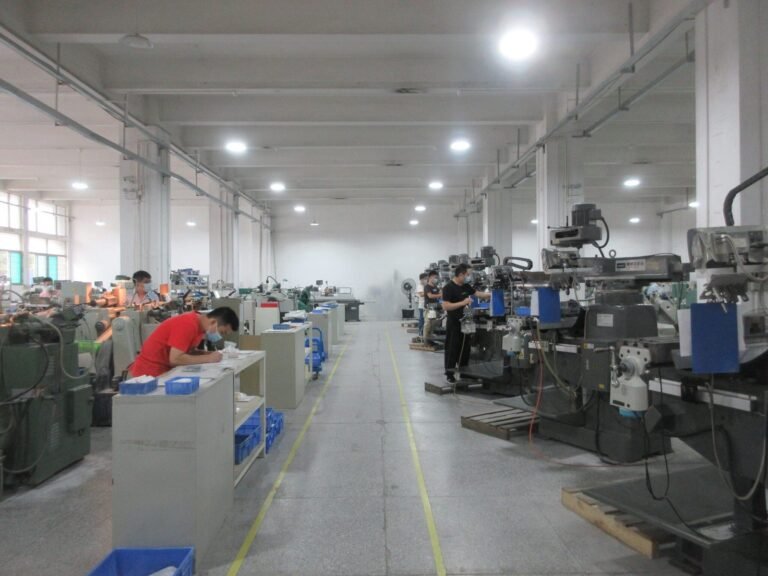
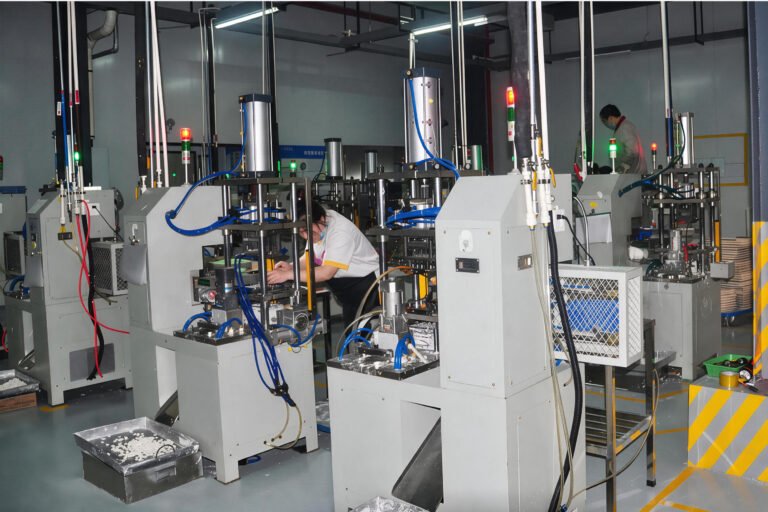
- Turned, milled, drilled and tapped with standard carbide tooling on conventional machines
- No firing step after machining, so the finished dimension is the machined dimension and no shrinkage allowance is needed
- Tapped holes and thin webs are practical, which is where the grinding route struggles
- Cutting fluid is used, so the process is familiar to any machine shop rather than being a specialist ceramic process
What to expect on the drawing
Tolerance and finish are specified per feature. An overall callout on the whole part is the most common cause of an unnecessarily expensive quotation.
Tolerance considerations
- General machining tolerances are straightforward because there is no firing shrinkage to compensate for
- The confirmed capability figures apply here too: hole diameter tolerance to 0.003 mm, roundness to 0.0005 mm and parallelism to 0.002 mm are achieved by grinding rather than milling, so a tight callout on a machinable part still moves the part to a grinding operation
- Threaded features are practical and are agreed as part of the review rather than assumed
Surface finish considerations
- As-machined finish is finer than an as-ground ceramic finish, which is often the reason it is chosen
- Polishing is straightforward where a sealing or optical surface is required
- Because the material is soft, surface damage during handling is the main risk rather than machining damage
Confirmed capability figures
The figures below are this shop’s confirmed manufacturing capability, quoted in this material’s context. They are feature-specific capability references, not blanket tolerances for every material or geometry.
These values are feature-specific capability references, not blanket tolerances for every material or geometry. Achievability depends on material, part size, wall thickness, feature geometry, datum scheme and finishing process. Final capability is confirmed during drawing review.
The machining route behind these figures is described under precision grinding, and the equipment that verifies them under inspection and metrology.
What is produced in this material
Component types only. No customer names are published.
Prototype insulator bodies
Vacuum chamber feedthrough components
Test fixtures and locating blocks
Laser and optical mounting spacers
Thermal break bushings
Profiled prototype bodies machined from solid
Instrument fittings and adaptor bodies
Custom insulating blocks with tapped features
Machinable Ceramics in service
The sectors below are the ones that specify this material, with the component that carries the requirement and the material property that earns the place. Each entry opens the sector page for the full component list.
A sector that is not listed is not a sector that is refused. It means the material has not been the obvious answer there, and the review starts from the operating condition instead.
How critical features are verified
A machinable grade is inspected like any other precision part; the difference is that internal features are more often accessible.
- General dimensions are measured with micrometers, height gauge and CMM
- Internal features that were machined rather than ground are checked on the video system
- Surface finish is measured where the drawing calls it out
- Threads and tapped features are checked with gauge tools agreed at drawing review
The equipment behind these methods is listed on the inspection and metrology page.
What to compare it against
These are the alternatives that most often come up against Machinable Ceramics, with the reason each might be preferred.
Technical documents
No file on this page is offered as a download, because each document is generated against the grade and the drawing on the order. What can be issued, and when, is listed here instead.
| Document | Applies to | Format | Issued |
|---|---|---|---|
| Material grade certificate | The grade the part is produced from | With the shipment | |
| Dimensional inspection record | The dimensions called out on the drawing | With the shipment | |
| Certificate of conformity | The finished part, against the drawing | With the shipment | |
| First article inspection report | The first part produced to a new drawing | On request; method agreed at quotation | |
| Material property data for the selected grade | The grade in question | On request, or from the material manufacturer |
A document that is not on this list is not refused by default; it is quoted once the method behind it has been confirmed. State what your incoming inspection will check, and the document set is agreed before the order is placed.
The part and the process
Frequently asked
How does it compare in strength with alumina?
It does not compare. Flexural strength of 108 MPa against 300 to 380 MPa for alumina means it is chosen where machining simplicity matters more than load carrying, and not the other way round.
Is machinable ceramic suitable for vacuum service?
Yes, and it is one of the better ceramics for it. Gas permeability is published as zero for this grade and water absorption is 0.00%, so there is no trapped volume to outgas.
What is the maximum service temperature?
800 °C. Above that the choice moves to alumina or boron nitride, depending on whether the atmosphere is air or inert gas, because boron nitride reaches 2000 °C in inert gas against 850 °C in air.
Need This Material for a Custom Component?
Send the drawing, the material grade if it is fixed, the quantity, the critical dimensions and tolerances, the required surface finish and the operating environment. The material is confirmed in writing with the quotation.